Cp vs Cpk: Differences, Formulas, Examples, and Acceptable Values
Written by Amrep’s Supplier Quality Engineering Team, last updated in September 2026
Cp and Cpk are process capability indices that measure how well a manufacturing process meets its specification limits. Cp evaluates the process spread relative to the tolerance width, calculated as (USL - LSL) / 6σ, while Cpk also accounts for process centering, calculated as the lower of (USL - μ) / 3σ and (μ - LSL) / 3σ.
The distinction matters in practice. A process with a Cp and Cpk of 1.67 retains the same Cp if its mean shifts toward one limit, yet its Cpk can fall to 1.00. Most customers require a minimum Cpk of 1.33 for ongoing production, while PPAP initial studies typically require a Ppk above 1.67.
This guide covers the differences, formulas, worked examples, and acceptable values for Cp and Cpk, along with how to improve and verify them.
What Is Process Capability?
Process capability is the ability of a stable process to produce parts within its specification limits. It compares two things: the voice of the customer, expressed as specification limits on the drawing, and the voice of the process, expressed as its natural variation.
Specification limits and control limits are not the same. Specification limits come from the customer or design engineer. Control limits come from the process data itself and show whether the process is stable.
Capability indices belong to Statistical Process Control (SPC), one of the AIAG core tools used alongside APQP, FMEA, MSA, and PPAP. Suppliers submit capability studies as evidence that a new process can hold the tolerance before production approval.
What Is Cp?
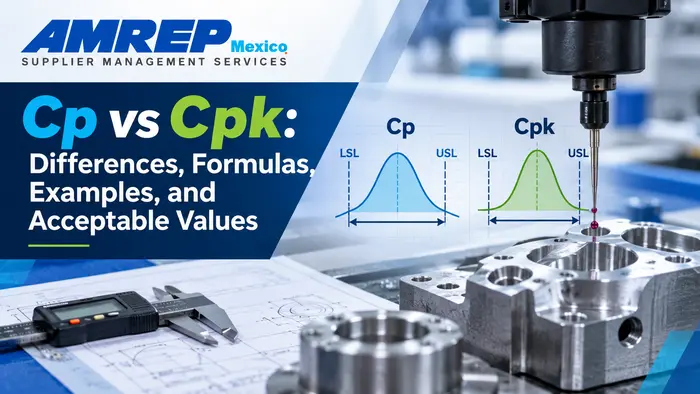
Cp is the potential capability index. It asks one question: if this process were perfectly centered, would its spread fit inside the tolerance?
A simple way to picture it is a car and a garage. Cp compares the width of the car to the width of the garage, but it ignores where the car is parked.
That is also its main limitation. A process can have an excellent Cp and still produce defects if the mean sits close to one limit.
Cp Formula
Cp = (USL - LSL) / 6σ
- USL is the upper specification limit
- LSL is the lower specification limit
- σ is the within-subgroup standard deviation
The denominator uses 6σ because roughly 99.73% of the area under a normal distribution falls within 3 standard deviations on either side of the mean.
What Is Cpk?
Cpk is the actual capability index. It measures how many 3-sigma units fit between the process mean and the nearest specification limit.
Because it only looks at the side of the distribution nearest a limit, Cpk reflects where defects are most likely to appear. Returning to the garage example, Cpk checks whether the car is parked close enough to one wall to scrape it.
Cpk Formula
Cpk = min [(USL - μ) / 3σ, (μ - LSL) / 3σ]
The formula breaks into two parts:
- CPU = (USL - μ) / 3σ, which measures capability against the upper limit
- CPL = (μ - LSL) / 3σ, which measures capability against the lower limit
Cpk takes the lower of the two. The weaker side decides how capable the process really is.
Cpu and Cpl for One-Sided Specifications
Some characteristics have only one limit. Flatness, runout, and burr height typically have a maximum only, while tensile strength or weld pull force typically have a minimum only.
For these features, Cp cannot be calculated because there is no tolerance width. Report Cpu for a maximum-only characteristic and Cpl for a minimum-only characteristic.
A common reporting error is inventing a second limit, such as zero, just to fill in a bilateral formula. This inflates the result and gives the customer a misleading number.
Cp vs Cpk: Key Differences
| Factor | Cp | Cpk |
|---|---|---|
| What it measures | Potential capability | Actual capability |
| Considers spread | Yes | Yes |
| Considers centering | No | Yes |
| Specification limits used | Both limits | Nearest limit |
| Works for one-sided specs | No | Yes, as Cpu or Cpl |
| Can be negative | No | Yes, if the mean falls outside a limit |
| Main decision it supports | Whether variation must be reduced | Whether parts meet spec today |
Reporting both indices together gives a complete picture. Cp alone hides centering problems, and Cpk alone hides whether the process even has the potential to be capable.
When Cp and Cpk are equal, the process is centered. The wider the gap between them, the further the mean has drifted from the middle of the tolerance.
Where Cpm Fits
Cpm, sometimes called the Taguchi index, goes one step further. It penalizes any distance between the process mean and the target value (T), not just the distance to a limit.
Cpm = (USL - LSL) / 6√(σ² + (μ - T)²)
Cpm is useful when a customer cares about hitting nominal, such as for mating fits or sealing surfaces. Most automotive PPAP submissions still rely on Cpk and Ppk.
How to Calculate Cp and Cpk Step by Step
- Confirm the measurement system is acceptable through a Gage R&R study per the AIAG MSA manual. Measurement error inflates σ and drags both indices down.
- Confirm the process is in statistical control using an X̄ and R chart or an individuals chart. Capability numbers from an unstable process predict nothing.
- Collect enough data. The AIAG PPAP manual recommends at least 25 subgroups containing at least 100 individual readings, unless the customer specifies otherwise.
- Check the data for normality with a histogram and a normality test.
- Estimate within-subgroup sigma using the method in the AIAG SPC Reference Manual (2nd edition). For subgrouped data, use σ = R̄ / d2. For individual readings, use σ = MR̄ / 1.128.
- Calculate the process mean.
- Calculate Cp, CPU, CPL, and Cpk.
- Compare the results against the customer requirement on the drawing, control plan, or supplier quality manual.
The d2 constant depends on subgroup size:
| Subgroup size (n) | d2 |
|---|---|
| 2 | 1.128 |
| 3 | 1.693 |
| 4 | 2.059 |
| 5 | 2.326 |
The sigma method must stay consistent. Comparing one supplier's Cpk calculated from R̄/d2 against another supplier's Cpk calculated from overall standard deviation is not a fair comparison.
How to Calculate Cp and Cpk in Excel
Excel can handle a full capability calculation with standard functions. Place your readings in one column, subgroup ranges in another, and enter USL, LSL, and the mean in named cells.
| What you need | Excel formula |
|---|---|
| Process mean | =AVERAGE(Data) |
| Within sigma (subgroups of 5) | =AVERAGE(Ranges)/2.326 |
| Overall sigma (for Pp and Ppk) | =STDEV.S(Data) |
| Cp | =(USL-LSL)/(6*Sigma) |
| Cpk | =MIN((USL-Mean)/(3Sigma),(Mean-LSL)/(3Sigma)) |
| Expected PPM for your actual mean | =(NORM.DIST(LSL,Mean,Sigma,TRUE)+1-NORM.DIST(USL,Mean,Sigma,TRUE))*1000000 |
The PPM formula above calculates both tails using your real mean, so it stays accurate when the process is off center. This avoids the common error of doubling a one-tail result.
Excel does not check stability or normality for you. Build a control chart first, and treat spreadsheet results as preliminary until the data passes both checks.
Cp and Cpk Worked Examples
The three examples below use an illustrative machined shaft, not a specific client case. Each scenario changes one variable so you can see how the indices react.
All three share the same specification: shaft diameter 25.00 ± 0.05 mm, giving an LSL of 24.95 mm and a USL of 25.05 mm.
Example 1: Centered and Capable
- Process mean = 25.00 mm, σ = 0.01 mm
- Cp = 0.10 / 0.06 = 1.67
- CPU = 0.05 / 0.03 = 1.67, CPL = 0.05 / 0.03 = 1.67
- Cpk = 1.67
At 1.67, the expected defect rate is below one part per million. If the overall variation matches the within-subgroup variation, the equivalent Ppk would also reach 1.67 and satisfy the AIAG PPAP default for an initial study.
Example 2: Tight Spread, Off-Center Mean
- Process mean = 25.02 mm, σ = 0.01 mm
- Cp = 0.10 / 0.06 = 1.67
- CPU = 0.03 / 0.03 = 1.00, CPL = 0.07 / 0.03 = 2.33
- Cpk = 1.00
The spread is identical to Example 1, yet Cpk dropped to 1.00 because the mean shifted 0.02 mm toward the upper limit. Expected rejects climb to roughly 1,350 PPM, almost all oversize.
Cpm with a target of 25.00 mm falls to about 0.75, which shows how strongly a nominal-focused customer would penalize this shift. The fix is recentering through a tool offset or fixture adjustment, not a more precise machine.
Example 3: Centered Mean, Too Much Variation
- Process mean = 25.00 mm, σ = 0.015 mm
- Cp = 0.10 / 0.09 = 1.11
- CPU = 0.05 / 0.045 = 1.11, CPL = 0.05 / 0.045 = 1.11
- Cpk = 1.11
Centering is fine here, but the spread is too wide. Expected rejects reach roughly 870 PPM, split across both limits.
Recentering will not help. The supplier needs to reduce variation by addressing tool wear, clamping repeatability, spindle condition, or material lot consistency.
How to Read Cp and Cpk Together
One part and one tolerance produced three different stories. The relationship between the two indices points directly to the corrective action.
| Pattern | What it means | Where to act |
|---|---|---|
| Cp high, Cpk high | Capable and centered | Maintain controls and monitor |
| Cp high, Cpk low | Spread is fine, mean is off center | Adjust the process mean |
| Cp low, Cpk low, both roughly equal | Centered but too variable | Reduce variation |
| Cp low, Cpk much lower | Off center and too variable | Recenter first, then reduce variation |
| Cpk negative | Mean sits outside a limit | Contain immediately and sort stock |
Recentering is usually faster and cheaper than variation reduction. Start there whenever the gap between Cp and Cpk is large.
Cp and Cpk vs Pp and Ppk
| Index | Variation used | Centering considered | Typical stage |
|---|---|---|---|
| Cp | Within subgroup (short term) | No | Ongoing production |
| Cpk | Within subgroup (short term) | Yes | Ongoing production |
| Pp | Overall (long term) | No | Initial study |
| Ppk | Overall (long term) | Yes | PPAP initial study |
Cp and Cpk use sigma estimated from variation inside each subgroup. Pp and Ppk use the overall standard deviation of all data, which includes shifts and drifts between subgroups.
When a process is in statistical control, Cpk and Ppk come out close to each other. A large gap means the process shifts between shifts, setups, or material lots, and that between-subgroup variation should be the first improvement target.
These indices feed directly into the initial process study element of a Level 3 PPAP submission, where customers review both the numbers and the supporting data.
What Are Acceptable Cp and Cpk Values?
| Cpk value | Interpretation | Typical application |
|---|---|---|
| Below 1.00 | Not capable | Containment and 100% inspection required |
| 1.00 to 1.33 | Marginal | Improvement plan required |
| 1.33 | Common minimum | Ongoing production in many industries |
| 1.67 | Highly capable | Initial studies and special characteristics |
| 2.00 | Six sigma level | Occasionally specified for critical features; confirm in the CSR |
These are conventions, not universal rules. The controlling requirement is always the customer's supplier quality manual, customer-specific requirements (CSRs), drawing notes, or control plan.
PPAP Default Acceptance Criteria
The AIAG PPAP manual (4th edition) sets default criteria for initial process studies when the customer has not specified otherwise:
- An index above 1.67 meets acceptance criteria
- An index from 1.33 to 1.67 may be acceptable, but the supplier must contact the customer for review
- An index below 1.33 does not meet acceptance criteria
Initial studies are usually evaluated with Ppk, not Cpk. Submitting the wrong index is a frequent reason capability studies get sent back.
IATF 16949 and OEM Specific Requirements
IATF 16949 clause 9.1.1.1 requires process studies on all new manufacturing processes to verify capability. It does not set a single threshold. Instead, it points suppliers to the customer's part approval requirements.
That is where OEM documents take over, and they differ:
- Ford's PPAP CSR requires Ppk above 1.67 to demonstrate final process capability at PPAP Phase 3. If 25 subgroups cannot be collected, Ford treats capability as undefined and requires 100% inspection or mistake-proofing.
- Ford's CSR has also required ongoing capability to be maintained at Ppk above 1.33.
- GM requires compliance with the AIAG PPAP manual and adds its own clauses on top.
- Stellantis publishes its own CSR for use with IATF 16949, which suppliers should check characteristic by characteristic.
In a plant supplying several OEMs, each characteristic must meet the strictest applicable requirement. Always read the CSR alongside the customer scorecard before accepting a supplier's study, and confirm during ISO and IATF audits that capability studies are built into the supplier's quality system.
Acceptable Values by Industry
| Industry | Governing documents | Capability expectation |
|---|---|---|
| Automotive | IATF 16949, AIAG PPAP and SPC manuals, OEM CSRs | Ppk above 1.67 at PPAP is common; 1.33 for ongoing production |
| Aerospace engines | AS9145, AS13100, RM13006 | Minimum Cpk of 1.33, with a Ppk target of 1.33 under AS13100 |
| Medical devices | ISO 13485:2016 clause 7.5.6, ISO 14971, FDA QMSR | No fixed regulatory value; criteria must be risk-based, and 1.33 is widely used |
| Electronics | OEM supplier quality manuals | No sector-wide value; set by each customer |
Medical device manufacturers deserve a specific note. The FDA's QMSR, effective February 2, 2026, incorporates ISO 13485 by reference, and neither sets a Cpk number. Acceptance criteria must be justified by the risk of the characteristic, so a high-severity feature may require well above 1.33.
Cpk to PPM Conversion Table
| Cpk | Sigma distance to nearest limit | Approx. PPM (centered, two-sided) |
|---|---|---|
| 0.67 | 2σ | 45,000 |
| 1.00 | 3σ | 2,700 |
| 1.33 | 4σ | 63 to 66 |
| 1.67 | 5σ | 0.57 |
| 2.00 | 6σ | 0.002 |
These figures assume a centered, normal, stable process. When the mean sits near one limit, nearly all defects fall on that side, so the realistic PPM is roughly half the two-sided figure. The 3.4 PPM often quoted for six sigma adds a 1.5 sigma long-term shift.
How Much Variation Reduction It Takes to Move from 1.33 to 1.67
At constant centering, Cpk rises in direct proportion to how much σ falls. Moving from 1.33 to 1.67 requires cutting σ by about 20% (1.33 ÷ 1.67 ≈ 0.80).
This gives suppliers a concrete improvement target. A 20% sigma reduction is achievable through focused work on the top variation sources, but it rarely happens through minor adjustments alone.
Capability Requirements Across the Launch Lifecycle
Capability is not a single study. Requirements change as a part moves from machine buyoff to serial production, and each stage uses a different index.
| Stage | Index | Typical minimum | Data basis |
|---|---|---|---|
| Machine qualification | Cm, Cmk | 1.67 | At least 50 consecutive parts from one uninterrupted run |
| PPAP initial study | Ppk | Above 1.67 (AIAG default) | At least 25 subgroups and 100 readings |
| Launch containment | Ppk or Cpk tracked | Per CSR exit criteria | Production data during containment |
| Ongoing production | Cpk, or Ppk where the CSR requires it | 1.33 is common | Frequency set by the control plan |
| After major changes | Repeat the relevant study | Same as original | New study after relocation, major repair, or process change |
Machine Capability (Cm and Cmk)
Cm and Cmk isolate the machine from the rest of the process. The study runs one uninterrupted batch under controlled conditions, so operator, material, and tool change effects are excluded.
The formulas mirror Cp and Cpk, but the sigma comes from that short run. Bosch Booklet 9 and VDA Volume 4 set minimums of Cm and Cmk at 1.67 with at least 50 parts.
The higher bar is intentional. Once operators, material lots, and tool changes add variation, a machine starting at Cmk 1.67 has room to still deliver Cpk 1.33 in production.
European OEMs and their Tier 1 suppliers often request Cmk studies before PPAP. A draft AIAG and VDA SPC manual released for review in February 2026 renames these indices Pm and Pmk, matching ISO 22514-3, so expect both naming conventions in customer documents.
Capability and Launch Containment
New programs often run under GP-12 early production containment or an OEM safe launch plan, and struggling suppliers can land in controlled shipping. In each case, customers look for stable, capable data before releasing the supplier from added inspection.
This makes capability evidence a cost issue, not just a paperwork issue. Every week a supplier stays in containment adds inspection labor and delays exit.
Common Cp and Cpk Mistakes That Get Supplier Reports Rejected
Most rejected capability studies fail on method, not math. These are the errors quality engineers see most often.
- Calculating capability on an unstable process, which makes the index meaningless as a prediction
- Skipping MSA or using a gage whose resolution is too coarse for the tolerance
- Running the study on a pilot lot of 20 or 30 pieces instead of the required sample size
- Applying normal formulas to naturally skewed characteristics such as flatness, runout, or concentricity
- Reporting Cpk when the customer asked for Ppk
- Mixing sigma methods across suppliers, cavities, or reports
- Pooling multi-cavity or multi-spindle data into one study, which hides a bad cavity
- Using sorted or screened parts instead of raw production output
- Reporting a single Cpk value without a confidence interval
Sample size deserves extra attention. Using a standard approximation (Bissell's formula), a Cpk of 1.33 from 30 parts has a 95% lower confidence bound near 1.03. The same Cpk from 125 parts has a lower bound near 1.18. Small studies can pass on paper and fail in production.
For non-normal data, use a transformation such as Box-Cox or Johnson, or apply the percentile method described in ISO 22514. State the method used in the report.
How to Improve Cp and Cpk
The diagnostic table in the worked examples tells you which lever to pull first. Getting that choice right prevents weeks of effort on the wrong problem.
When the Problem Is Centering
A centering problem means the process can hold the tolerance but aims at the wrong point. The cause is usually setup-related: offsets entered from memory, worn locators, or first piece approval that only checks whether a part is in tolerance rather than near nominal.
Because the root cause sits in the setup routine, the fix must live there too:
- Verify tool offsets and setup sheets at every changeover
- Check fixture locating features for wear
- Require first piece approval against the nominal, not just the tolerance
- Add mean-based reaction rules to the control plan
Centering gains fade quickly if nobody checks the routine. Layered process audits help keep these setup controls from slipping after the initial fix.
When the Problem Is Variation
A variation problem means the process cannot hold the tolerance no matter where it aims. The causes are spread across the process, so single adjustments rarely work, and structured analysis is required.
- Map variation sources with a fishbone diagram and 5 Why analysis
- Use design of experiments to isolate the parameters that drive spread
- Tighten preventive maintenance on spindles, fixtures, and tooling
- Control incoming material lots and document operator standard work
Variation reduction is where structured quality methods like Total Quality Management and Lean Six Sigma earn their value. The work is slower than recentering, but the gains hold when they feed an ongoing QA performance improvement program.
How to Verify Supplier Cp and Cpk Data in Mexico
A capability report is only as reliable as the study behind it. OEMs sourcing from Mexico often approve new suppliers based on documents alone, then discover the real process performance during launch.
On-site verification through supplier factory audits closes that gap. A supplier quality engineer on the floor can confirm what a report cannot show.
What to Check on the Shop Floor
Floor checks confirm that the study reflects normal production rather than a controlled demonstration.
- Gage condition, calibration status, and Gage R&R results
- Whether study parts came from normal production at rate
- The raw data trail, including subgroup timestamps
- Control chart history before and after the study
- Whether the operator measurement method matches the control plan
Red Flags in Submitted Capability Reports
Some patterns in a report deserve a closer look before approval.
- Identical Cpk values across different characteristics or studies
- Perfectly shaped normal histograms from very small samples
- Missing subgroup data or only summary statistics provided
- Capability reported without evidence of MSA
- Very high values, such as Cpk above 3.00, which should prompt a check of the specification limits, units, and decimal placement used. A loose tolerance can legitimately produce a high Cpk, so treat this as a verification step, not a rejection.
Frequently Asked Questions
What is a good Cp value?
A Cp of 1.33 or higher is generally considered good, since the tolerance is at least 1.33 times wider than the process spread. Cp only shows potential, so always check Cpk to confirm the process is also centered.
Why is my Cpk low when all parts are in spec?
Cpk predicts future output, not just the parts you measured. If the spread sits close to a limit, future parts will fall outside it even though your sample did not. A coarse gage or an unstable process can also push the index down.
How do you convert Cpk to sigma level?
Multiply Cpk by three. A Cpk of 1.33 equals a four sigma process, 1.67 equals five sigma, and 2.00 equals six sigma.
What is Cmk and how is it different from Cpk?
Cmk measures machine capability from one short, uninterrupted run of at least 50 parts. Cpk measures process capability over time, including operators, materials, and tool changes. Cmk minimums are usually higher (1.67) to leave room for that added variation.
How often should Cpk be recalculated?
Follow the frequency in your control plan and the customer's CSR. Recalculate after any machine relocation, major repair, tooling change, material source change, or process change.
Can you calculate Cpk for attribute data?
No. Cp and Cpk require continuous measurement data. For pass or fail characteristics, capability is expressed as a defect rate in PPM or DPMO, typically tracked on a p chart or np chart.
Can Cpk be too high?
Not from a quality standpoint, but a very high Cpk can signal cost. The process may be more precise than needed, or the tolerance may be looser than the design requires. Both are worth reviewing with engineering.
Get Reliable Capability Data from Your Mexican Suppliers
Capability numbers drive approval, launch, and containment decisions, so they need to be accurate. AMREP Supplier Quality Management Services places experienced engineers directly in Mexican supplier plants to verify capability studies, trace the variation sources behind low Cpk, and bring processes up to your customer requirements.
Whether you are approving a new supplier or pushing an existing process from 1.33 to 1.67, you can work with our supplier quality engineers to get capability data that reflects how parts are actually made.